A buyer asked three factories for sanitary pad production capacity per day and received three numbers. All three were honest. None were comparable, because one was counted at the forming machine, one at the bagger, and one at the carton sealer, each on a day with a different number of running products. Capacity per day is not a property of a machine. It is the arithmetic of a schedule that has not been written yet.
Why Sanitary Pad Production Capacity Per Day Is a Schedule Question
A nameplate figure describes the machine at one product, with stable material, while nothing else interrupts it. A day is not that. A day contains stops, a speed that is held or not held, and output that is rejected or reworked. Any factory that tracks these three separately reports them separately; a single daily figure merges them into one number nobody can audit afterwards.
That is why the question is only answerable as a day shape: which products run, in what order, at which counting point, and with what qualification discipline. Change any one of those four and the answer moves without a bolt being touched on the line.
The consequence is uncomfortable for both sides. A supplier who answers a bare per-day question is guessing at your schedule. A supplier who answers with conditions is telling you the truth, and it reads like evasion until you have compared two such answers side by side.
Three Counting Points, Three Different Numbers
One line offers at least three legitimate places to count. They differ by how much work has already been added to the unit, and by how much buffer sits between them.
| Counting point | What the figure includes | What it leaves out |
|---|---|---|
| Forming machine output | Units formed and cut, before wrapping | Wrap, pouch, carton, and any unit scrapped at packing |
| Bagged packs | Sealed packs that passed the pack seal check | Cartons, pallet pattern, and packs rejected at final check |
| Sealed cartons | Cartons closed, labelled, and counted against the packing list | Pallets not yet wrapped, and units still in rework |
Between the bagger and the cartoner there is usually a buffer, so the two ends of one line can drift apart inside a single shift. A figure quoted at the forming machine and a figure quoted at the carton sealer can both be accurate on the same day and still differ by the size of that buffer.
The counting point that matters commercially is the one where goods become both saleable and checkable. For most export orders that is the sealed carton, because that is what the packing list counts and what the container is loaded by, which is also why wholesale orders are usually priced against it rather than against machine output.
Changeover Is a Fixed Block, Not a Rate
A sanitary pad production line changeover is not a percentage penalty on the day. It is a block of machine time: rolls changed, forming parts swapped for the new size, sealing profile reset, adhesive re-set, then a run until the first units match the approved sample. The block is roughly fixed, which is why sanitary pad production capacity per day behaves as a step function rather than a slope.
Two products in a day and three products in a day do not differ by a third of the output. They differ by one whole block plus the ramp-up scrap that block throws away. This is the mechanism behind something buyers notice but rarely name: a factory running one product for a week looks far quicker than the same factory running three.
It is also why a narrow range is cheaper to keep in stock than a wide one, even when every unit costs the same to make. The block is paid whether or not the volume justifies it, and that is what a minimum order quantity is really pricing.
The Ramp-Up Block Nobody Counts
After the mechanical changeover the line is running, but it is not qualified. The first-off units are compared with the approved sample on thickness, seal appearance, fold position and print registration. Until that comparison passes, output is not shippable, so the qualification block is capacity the machine has and the plan does not.
Qualification is a decision, not a duration. Two factories with the same hardware can differ by half a shift here, because one has a written comparison and signs it off, and the other waits for whoever is senior to walk over. Neither will call this capacity, and both feel it every day.
The reason to care is that this third term grows with how different the new product is. A size change inside one construction is a short block. A change of absorbent structure, film or fold is a long one, because the comparison has more places to fail.
Packing Sets the Ceiling Before the Machine Does
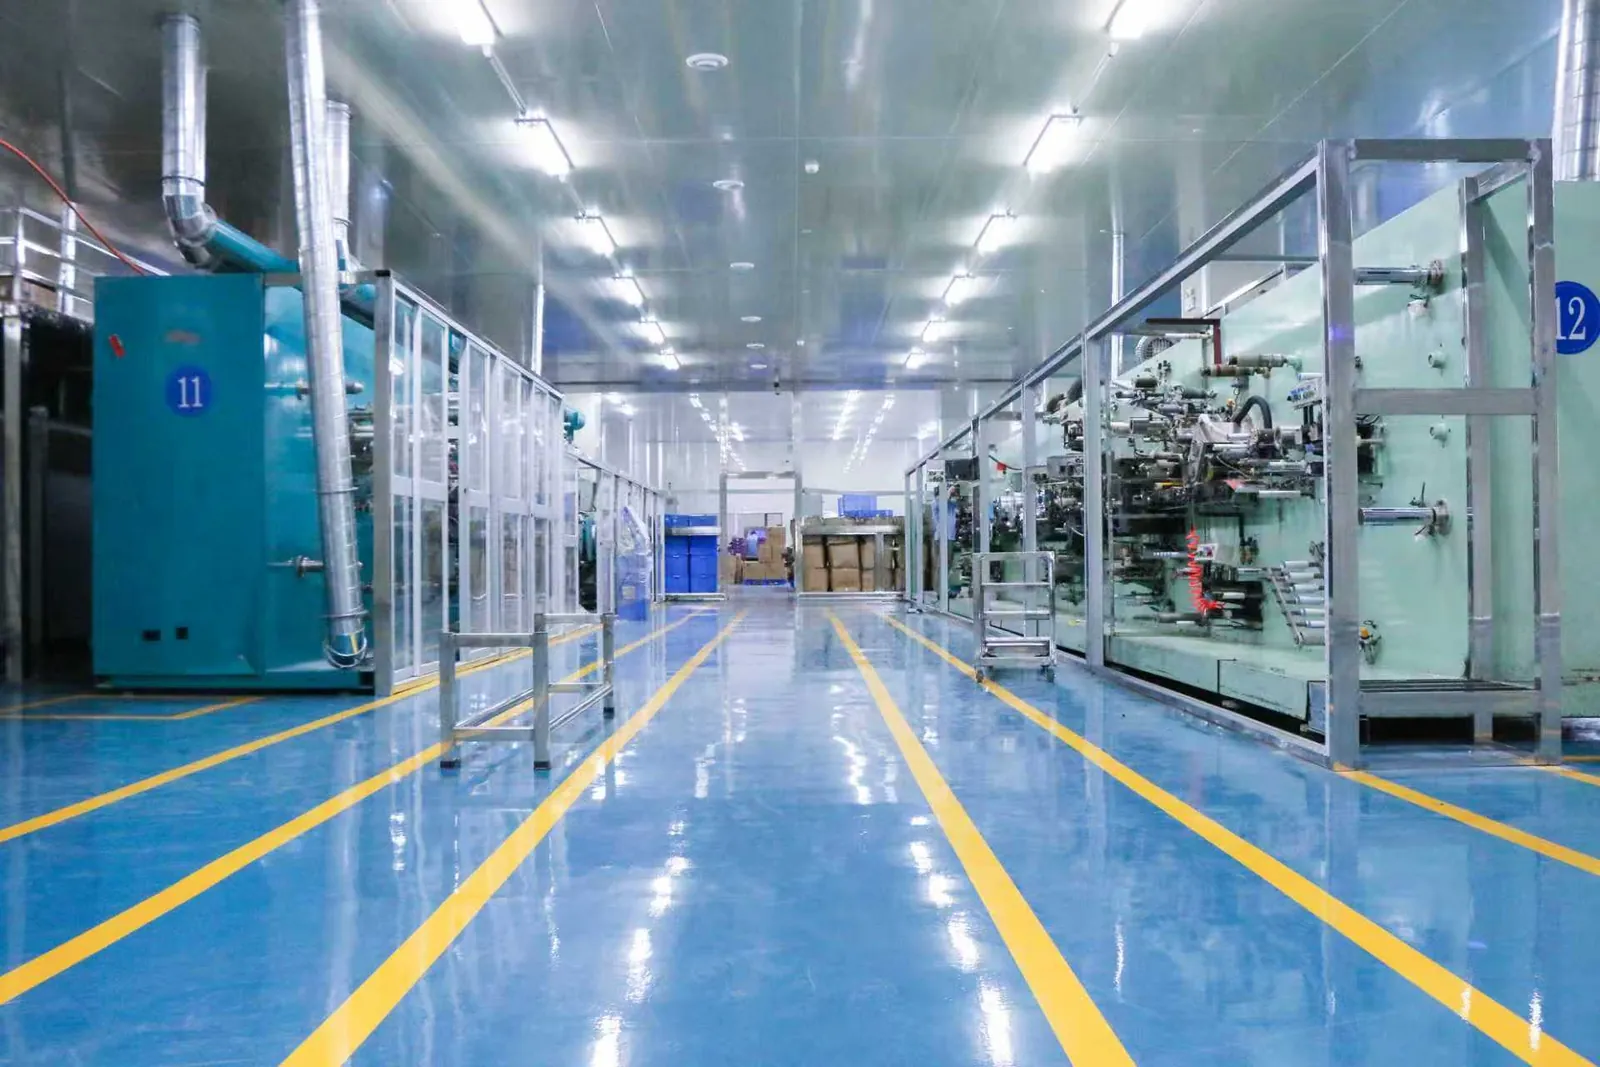
A sanitary pants production line is usually bounded further downstream than buyers expect. The forming and sealing section can outrun the stations that bag, count and case the units, because those carry more handling per unit. When that happens the honest daily figure belongs to packing labour and to the carton plan, not to the machine.
The carton plan is a decision with arithmetic consequences. Packs per carton, cartons per layer, layers per pallet: change the first and the same unit output becomes a different number of cartons, a different number of pallets and a different container load. Nothing on the line changed, and the number did.
So a daily figure quoted in cartons should always be read next to the pack count it assumes. Without that second number the figure is a unit conversion waiting to be misread, and misreading it is how a launch lands a month late.
What Sampling Does to the Arithmetic
The sanitary pad quality inspection process is a schedule element, not a gate at the end. It runs on an acceptance sampling plan, so the units taken and the time spent depend on lot size and on the accept or reject decision, not on machine speed.
A reject decision is an availability event. It stops the run, it triggers a hold, and it moves that day of output into a state that is neither shippable nor scrap until somebody decides. Buyers who treat inspection as something added after production are assuming that decision never lands.
The useful question is therefore not how much gets inspected but where the hold sits and who releases it. That answer tells you what a bad hour costs, which is a capacity question wearing a quality label.
Reading a Figure Against Your Own Dispatch Calendar
A day is machine time, not twenty-four hours. Planned maintenance, cleaning between products, shift handover and the holiday calendar all sit inside the same window. A figure that assumes uninterrupted running is a design figure again, dressed up as a commitment.
Dispatch rhythm matters as much. If containers are consolidated weekly, daily output has to be buffered until the loading day, and buffer space becomes the constraint that stops the line. A floor with full pallet positions is not going to run at its nameplate figure for long.
Read against a calendar, a range says more than a single number, because the range shows which days are clean and which carry a changeover. That shape is what a launch plan is actually built from, and it is the part of factory capability worth asking about first.
How to Ask So Two Answers Compare
The question that produces comparable answers is not how many per day. It is what a normal week looks like for this product mix, counted at sealed cartons, with changeover blocks shown separately. Five details make that answer usable:
- The product list, with construction and size for each item.
- Pack count per carton and cartons per pallet, so the unit conversion is fixed.
- The counting point you will accept, written into the order.
- The month you intend to load, because the calendar is part of the answer.
- Permission to name the constraint step, which is often packing rather than forming.
We ship from China, so the day shape we describe is the one our own schedule produces rather than an average borrowed from a brochure. Send the product list and the loading month, and we will return the blocks, the counting point and the step that becomes the limit first, through our contact page. That is a more useful document than a headline number for sanitary pad production capacity per day, and it is the one you can hold a supplier to.
Frequently Asked Questions
Does daily capacity change when the product size changes?
Yes. A size change means the forming parts and the sealing profile change, and the run is not qualified until the first-off units match the approved sample. The block is shorter than a full construction change, but it is still machine time that cannot be recovered later in that shift.
Which counting point should a purchase order name?
Name the point where the goods become both saleable and checkable, which is normally the sealed carton, and state the pack count per carton beside it. Without that second detail the same unit output converts into a different number of cartons, and the figure cannot be checked on arrival.
Can one daily figure hold for a whole season?
No, because the figure belongs to a product mix rather than to the factory. A season with three running products carries three changeover blocks and their ramp-up scrap. Ask for the mix and the block sizes, and the day follows from the arithmetic instead of from a promise.
Why do two factories with the same machine speed quote different days?
Three usual reasons: they count at different points on the line, they qualify the run differently after a changeover, and their packing stations carry different handling per unit. None of the three shows up in a speed figure, and all three change the day.
What should a buyer send to get a comparable answer?
The product list with construction and size, the pack count per carton, the month you intend to load in, and the counting point you will accept in the order. With those four a supplier can return a day shape rather than a single number, and you can compare it with a second factory.