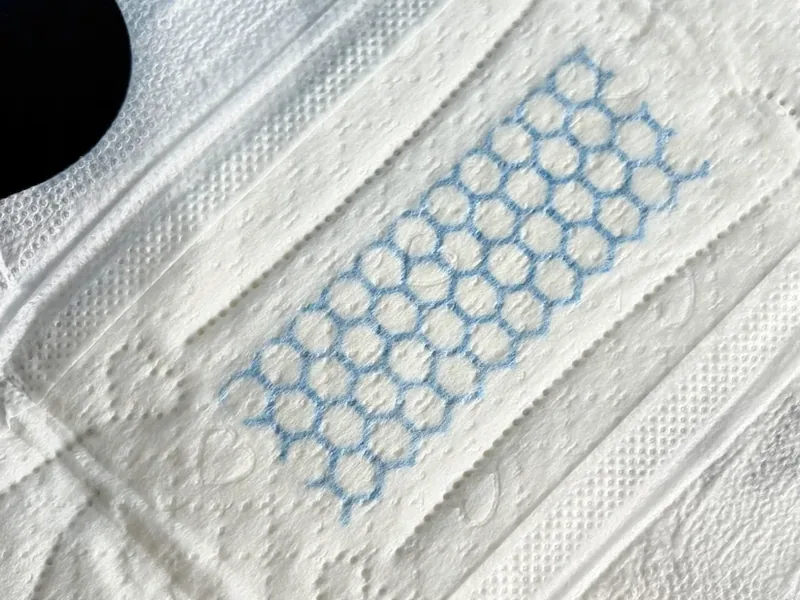
Side-seam menstrual pants exist because the garment can be opened flat and positioned without stepping into it. That function depends entirely on one joint: the seam. And the seam is the part of the product most exposed to a speed-versus-quality trade-off.
What the seam has to do
The seam must hold under three different loads: tension along its length when the pant is worn, peel force across its width when the wearer moves, and shear during handling and packing. It must also feel flat against skin, because a ridge at the hip is a comfort complaint.
Three sealing methods are used in the category:
- Ultrasonic welding. Energy is applied through a horn and anvil; the material fuses. Fast, no consumable, and highly sensitive to gap and pressure.
- Thermal sealing. Heat and pressure with a dwell time. Simpler to control, slower, and prone to marking.
- Adhesive seaming. Hot-melt bond. Flexible and low-profile, but depends on the same humidity behaviour as any other adhesive joint.
Where speed enters the equation
Every one of those methods depends on dwell time — the fraction of a second the material spends under energy and pressure. Run the line faster and dwell shortens. If nothing else changes, the joint receives less total energy and the bond weakens.
A line can be pushed faster if the energy input is raised to compensate. That works up to a point, and the point is where the material starts to fail instead: over-welded nonwoven becomes brittle, and brittle seams crack rather than stretch. The failure moves from a peel failure at low energy to a tear failure at high energy, and both are rejects.
The practical window is narrower than the nominal line speed suggests, which is why a quoted capacity and a quoted seal strength should be read together.
How seal integrity is actually checked
Destructive peel testing on cut samples is the standard method: a defined strip is peeled at a controlled rate and the peak force recorded. This is a batch check, not a continuous one, so it catches setting errors rather than transient drift.
Two further checks are worth asking about:
- Visual inspection at the anvil. Continuous, operator-based, and effective at catching gross misalignment.
- Inline pressure or gap monitoring. Continuous and instrumented. Not universal, but the only method that detects drift between destructive samples.
Specifying a seam that survives wear
A purchase specification that says the pant is "side-opening" says nothing about the joint. Four items make it testable:
- Sealing method, and machine type where relevant.
- Target peel strength, with the test method and sample width stated.
- Seam position and width tolerance.
- Acceptance criteria for visual defects at the seam, defined rather than described as "neat".
This matters more for side-seam than for any other construction, because there is no second joint to share the load. The side-opening program page sets out how we specify the joint, and the side-seam versus pull-up comparison explains when the extra process step earns its cost.