Every sanitary pad quotation contains a materials figure, and inside that figure is an assumption about waste. Buyers rarely see it. It is usually buried as a percentage uplift on the raw material cost, and it is one of the few line items that changes materially with order size.
Understanding how trim waste behaves is the difference between a quote that holds and a quote that quietly gets renegotiated at the third shipment.
Where the waste comes from
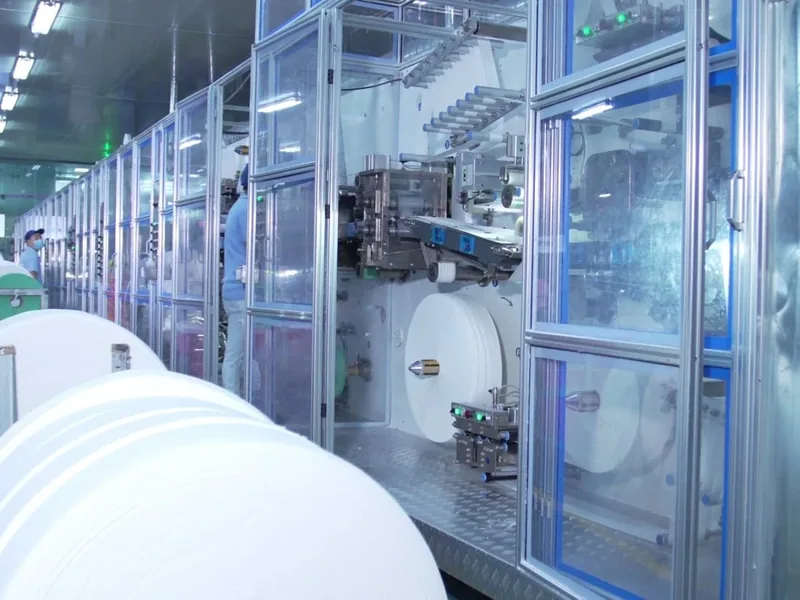
A pad line converts wide rolls into a narrow finished product. Material leaves the process in four ways:
- Edge trim. The width left outside the product profile. Set by format, not by operator skill.
- Start-up waste. The first metres of any run, until registration, tension and sealing stabilise.
- Changeover waste. Material consumed while the line is reconfigured between formats.
- Reject waste. Units that fail inline inspection and are removed.
Only the last of these responds meaningfully to operator attention. The first three are structural, and they are what actually determine the waste curve.
Why the curve is not a percentage
Start-up and changeover waste are fixed quantities in metres, not proportions. That produces a curve with a distinct shape:
On a short run, fixed waste dominates. Two hundred metres of start-up on a five-thousand-metre run is four per cent before a single unit is rejected. On a fifty-thousand-metre run the same two hundred metres is a rounding error.
This is why a factory can honestly quote nine per cent waste on a trial order and four per cent on a container programme, and why the second quote is not a discount — it is the same line behaving differently at a different length.
Edge trim behaves in the opposite way. It is proportional and it does not improve with volume. If the product width does not nest well into the roll width, that loss is permanent for that format.
The question that exposes the real number
Ask what roll width the format is being run from, and what the finished product width is. The ratio tells you the nesting loss immediately, and no amount of negotiation will move it.
A format that leaves a wide offcut is not necessarily a bad choice — it may be the only way to hit a required absorbency — but it should be a known cost rather than a surprise. Formats that nest efficiently are usually the ones a factory will steer you toward, and it is worth asking why when they do.
What to fix in the commercial terms
- State the waste assumption. A percentage with no volume context is not a commitment.
- Tie it to a run length. Waste at one container and waste at five containers are different numbers, legitimately.
- Agree how changeover is charged. Either absorbed into unit price or billed once per run — but say which.
- Decide who owns reject waste. Inline rejects caused by material defects should not land on the buyer's unit cost.
The quote and cost comparison guide sets out how these items usually appear in a Chinese factory quotation, and the manufacturing process page shows where each waste source sits on the line.
None of this is exotic. It is simply the part of the cost structure that stays invisible until someone asks.